Chevrolet Cruze Repair Manual: Removal Procedure
Warning: Refer to Approved Equipment for Collision Repair Warning in the Preface section.
Warning: Refer to Glass and Sheet Metal Handling Warning in the Preface section.
- Disable the SIR System. Refer to SIR Disabling and Enabling.
- Disconnect the negative battery cable. Refer to Battery Negative Cable Disconnection and Connection.
- Remove all related panels and components.
- Visually inspect the damage. Repair as much of the damage as possible.
- Remove the sealers and anti-corrosion materials from the repair area, as necessary. Refer to Anti-Corrosion Treatment and Repair;
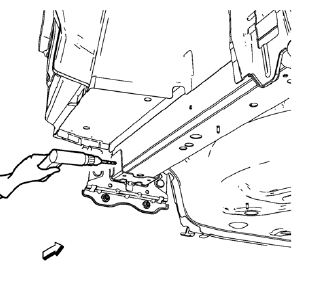
- Locate and mark all the necessary factory welds of the rear end panel plate.
Note: Note the number and location of welds for installation of the service assembly.
- Drill all factory welds.
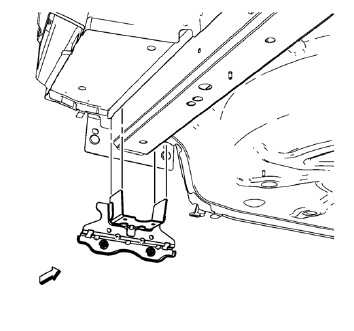
- Remove the underbody rear side rail reinforcement
 Underbody Rear Side Rail Reinforcement Replacement (MIG-Brazing)
Note: According to different corrosion warranties, only the
regional mandatory joining methods are allowed. ...
 Installation Procedure
Create 8 24 mm (5/16 x 15/16 in) slots for MIG-brazing along the edges
of the underbody rear side rail reinforcement as noted from
the original panel.
Clean and prepare the attaching&nb ...
Other materials:
Ignition Positions (Key Access)
The ignition switch has four different positions.
Notice: Using a tool to force the key to turn in the ignition could
cause damage to the switch or break the key. Use the correct key, make sure it is
all the way in, and turn it only with your hand.
If the key cannot be turned by hand, see yo ...
General Information
Your vehicle is an important investment. This section describes the required
maintenance for the vehicle. Follow this schedule to help protect against major
repair expenses resulting from neglect or inadequate maintenance. It may also help
to maintain the value of the vehicle if it is sold. It ...
Installation Procedure
Drill 8 mm (5/16 in) for plug welding along the edges of the front
wheelhouse front panel as noted from the original panel.
Drill 8 mm (5/16 in) for plug welding where front wheelhouse front panel
and front wheelhouse overlap.
Clean and prepare the attaching surfaces f ...
